Flanging Machine Technology Gains Attention as Fabricators Pair Precision Forming With Small Press Brake Flexibility
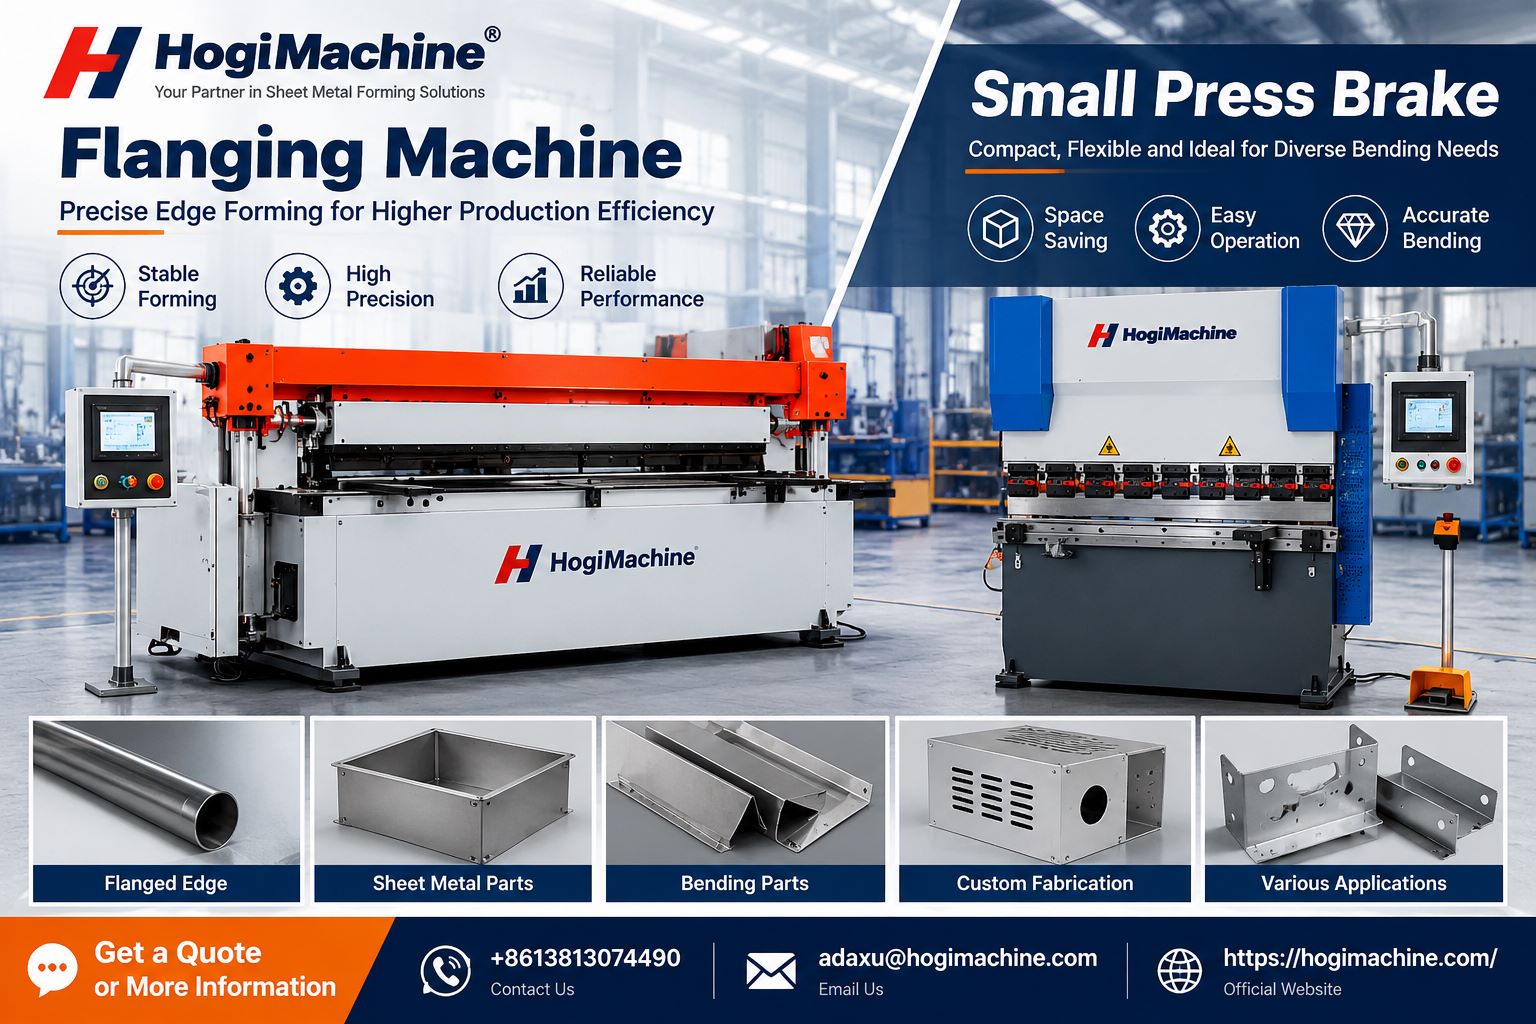
Sheet-metal manufacturers are placing greater emphasis on flexible forming equipment as production shifts toward shorter runs, customized components, faster changeovers, and tighter dimensional requirements. Instead of relying only on large general-purpose systems, workshops are increasingly combining specialized machines with compact forming equipment to improve workflow.
Within this trend, the Flanging machine is gaining attention for operations that require controlled edge forming, while the small press brake is becoming an increasingly practical choice for workshops handling compact components, prototypes, repair work, and lower-volume production.
Why Flanging Technology Matters in Modern Fabrication
Flanging is a metal-forming operation used to create an edge, lip, or flange on a workpiece. Depending on the application, the formed section can support assembly, joining, reinforcement, or subsequent manufacturing operations.
A Flanging machine is designed to make this operation more controlled and repeatable than relying on unsuitable general-purpose methods.
The correct equipment depends on the component geometry, material characteristics, thickness, flange requirements, production quantity, and expected accuracy.
For manufacturers, the objective is not simply to bend an edge. It is to achieve a repeatable form that fits correctly into the next stage of production.
Specialized Equipment Can Improve Production Flow
Fabrication shops often manufacture products involving several forming operations.
Some components may need cutting, edge preparation, flanging, bending, joining, and finishing before they are ready for assembly.
Using specialized equipment for recurring operations can help organize this workflow.
A Flanging machine can be integrated into a broader manufacturing process so that operators perform the required edge-forming operation without repeatedly setting up equipment intended for other tasks.
This can be particularly useful when similar components are produced regularly.
Small Press Brake Equipment Supports Flexible Manufacturing
While specialized machinery handles dedicated operations, compact bending equipment offers a different advantage: versatility.
A small press brake can be useful for bending smaller sheet-metal parts, producing brackets, forming short components, completing prototypes, and supporting maintenance or repair work.
For workshops with limited floor space, compact equipment may also provide a practical way to add bending capacity without dedicating the area required by a substantially larger machine.
The correct press brake should still be selected according to material, thickness, bend length, tooling, and required forming force.
Short-Run Manufacturing Is Changing Equipment Priorities
Traditional manufacturing models often emphasized long production runs. Today, many fabricators serve customers requiring smaller batches and more frequent design changes.
This creates different equipment requirements.
For short runs, setup time can represent a meaningful portion of total production time. Manufacturers therefore value equipment that can be prepared efficiently for the next job.
A small press brake can fit this production model when the parts fall within its suitable working range.
Rather than occupying larger equipment with small components, a workshop can allocate jobs according to machine capability and production priorities.
Tooling Selection Has a Direct Impact on Results
The machine itself is only part of the forming system.
Tooling geometry needs to match the material and intended component shape. Incorrect tooling can make it difficult to achieve the required result and may create unnecessary stress on equipment or workpieces.
For press brake operations, punch and die selection should be appropriate for the required bend and machine capacity.
Similarly, a Flanging machine should use suitable forming arrangements for its intended operation.
Manufacturers should establish clear setup procedures so operators understand which tooling is appropriate for recurring jobs.
Material Behavior Must Be Considered Before Forming
Different metals do not behave identically during forming.
Material type, thickness, mechanical characteristics, grain direction, and component geometry can all influence the result.
Springback is one factor that may need to be considered during bending. The workpiece can recover slightly after forming force is removed, affecting the final angle.
Production teams should therefore establish parameters based on the actual material and component requirements rather than assuming one setup will work for every job.
This is important for both specialized flanging operations and work completed on a small press brake.
Repeatability Is Essential for Assembly
A formed component rarely exists by itself.
It may need to fit into an enclosure, frame, cabinet, duct, machine, or another fabricated assembly. If bending or flanging varies significantly between components, downstream assembly can become more difficult.
Repeatable forming helps maintain alignment and fit.
Manufacturers can support consistency through controlled tooling, documented setups, appropriate measurement, machine maintenance, and operator training.
For recurring jobs, recording successful production settings can also make future setup more efficient.
Compact Equipment Can Improve Factory Layout
Floor space has economic value.
Workshops need room not only for machines but also for material storage, work-in-progress, inspection, assembly, and safe movement.
A small press brake can be attractive where the required components do not justify a larger forming system.
Compact machinery may also be positioned closer to related operations where appropriate, potentially reducing unnecessary movement of small workpieces.
Factory layout should still account for safe operating areas, tooling access, material handling, maintenance, and operator ergonomics.
Preventive Maintenance Supports Forming Accuracy
Forming equipment should be maintained systematically.
Wear, looseness, lubrication requirements, tooling condition, alignment issues, and other mechanical factors can affect both reliability and finished-component quality.
Routine inspection allows technical teams to identify developing problems before they create significant downtime.
A maintenance schedule for a Flanging machine should reflect its design, usage, and manufacturer guidance. The same principle applies to press brake equipment.
Maintenance records can provide useful information when diagnosing recurring production issues.
Frequently Asked Questions
What is a Flanging machine?
A Flanging machine is metal-forming equipment used to create a flange, lip, or formed edge on a workpiece for applications such as assembly, reinforcement, or joining.
What is a small press brake?
A small press brake is compact bending equipment designed for forming sheet-metal components within its specified working length and forming capacity.
Where is flanging commonly used?
Flanging can be used in different fabricated products where formed edges are required for structural, assembly, connection, or manufacturing purposes.
Why would a workshop use a compact press brake?
Compact equipment can provide dedicated capacity for smaller components, prototypes, short production runs, repair jobs, and other suitable bending work.
Can a small press brake bend every metal thickness?
No. Every machine has defined capacity limits. Material type, thickness, bend length, tooling, and required force should be considered before forming.
Why is tooling important in sheet-metal forming?
Suitable tooling helps create the required geometry while supporting consistent and controlled forming.
What causes springback?
Springback occurs when metal partially recovers after forming force is removed. Its extent depends on material and forming conditions.
How can manufacturers improve bending repeatability?
Controlled setups, suitable tooling, documented parameters, maintenance, measurement, and operator training can all support repeatable production.
Is compact machinery suitable for high-mix production?
It can be, particularly when component dimensions and forming requirements match the machine’s capabilities and frequent job changes are required.
What should buyers evaluate before purchasing forming equipment?
Buyers should consider component geometry, material, thickness, production volume, working dimensions, required force, tooling, accuracy expectations, available space, and technical support.
Media Contact
Sheet Metal Machinery & Equipment Enquiries
Email: adaxu@hogimachine.com
Contact: +8613813074490
Website: https://hogimachine.com/